OEKO-TEX Standard 100 is a globally recognized textile safety certification that tests fabrics, trims, and accessories for harmful substances to ensure they are safe for skin contact. For apparel brands and B2B buyers, it helps reduce compliance risk, meet retailer requirements, and build consumer trust—especially for products with direct skin contact.
This guide explains product classes, common restricted chemicals, how fabric safety testing works, key global regulations, and practical steps manufacturers use to manage RSLs and third-party lab reports before bulk production.In today’s global apparel market, safety compliance is becoming just as important as design, price, and manufacturing capability. Many clothing brands now integrate OEKO-TEX Standard 100 and safety verification into their production process to ensure consistent product quality.
Reduce Recall Risk with Fabric Safety Testing
Fabric safety testing plays a critical role in modern apparel production. It helps clothing brands ensure that garments meet international safety requirements and retailer compliance standards. Fabric testing is important because it helps:- Ensure garments are safe for skin contact
- Detect harmful chemicals in textile materials
- Meet international regulatory requirements
- Reduce product recall and compliance risks
- Improve brand credibility in global markets
What OEKO-TEX Standard 100 Covers in a Finished Garment
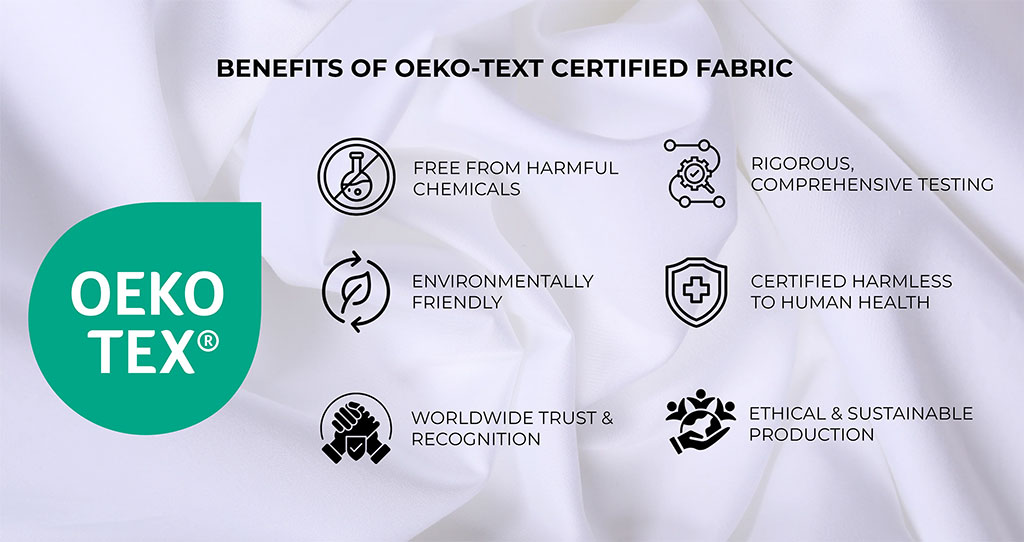
Among the certification systems developed by OEKO-TEX, the most widely used is OEKO-TEX Standard 100. This certification verifies that every component of a textile product has been tested for harmful substances. Unlike many certification programs that only evaluate fabrics, OEKO-TEX examines all materials used in the finished garment. These components may include:- Fabric materials
- Sewing threads
- Zippers and trims
- Buttons and accessories
- Labels and printed graphics
Apparel Compliance & QC Process Table
| Stage | What to collect | Who provides it | Output / Record |
| Material sourcing | Supplier certificate (ISO / factory profile) | Fabric supplier | Approved supplier list |
| SDS (Safety Data Sheet, if applicable) | Chemical / dye supplier | SDS archive | |
| Material composition declaration | Fabric supplier | Fiber composition record | |
| Restricted Substance List (RSL) compliance statement | Supplier | RSL compliance file | |
| Pre-production | Design specification (tech pack) | Brand / buyer | Tech pack archive |
| Bill of Materials (BOM) | Factory merchandiser | BOM record | |
| RSL confirmation | Factory + supplier | Signed RSL confirmation | |
| Sample testing request | Factory QA | Testing request form | |
| Lab test report for samples | Third-party lab | Sample test report | |
| Pre-production sample approval (PPS) | Buyer / brand | PPS approval record | |
| Bulk production | Incoming material inspection report | Factory QC | Incoming QC record |
| Batch / lot traceability | Factory production | Production batch record | |
| In-line production inspection | Factory QC | In-line inspection report | |
| Process control checklist | Factory production | Process control record | |
| Pre-shipment | Final random inspection (FRI) | Factory QC / third-party inspection | Final inspection report |
| Lab test report for bulk products (if required) | Third-party lab | Bulk test report | |
| Packaging verification | Factory QC | Packaging checklist | |
| Labeling compliance check | Factory QA | Label compliance record | |
| Shipment | Final QC approval | Factory QA | Shipment release note |
| Test report archive | Factory QA | Compliance archive | |
| Packing list / invoice | Export department | Shipping documents | |
| Batch traceability confirmation | Factory QA | Traceability record | |
| Post-shipment | Quality feedback / complaint record | Buyer / customer | CAPA report |
| Corrective action report (if issue occurs) | Factory QA | Corrective action record | |
| Compliance document archive | Factory compliance team | Long-term compliance file |
Choose the Right Product Class for Your Clothing Line
OEKO-TEX Standard 100 categorizes textile products based on how closely they come into contact with human skin.Product Class I – Baby Products
This category includes textiles designed for infants and toddlers under three years old. Safety requirements are extremely strict. Examples include:- Baby clothing
- Infant bedding
- Soft toys
Product Class II – Direct Skin Contact
Products that have frequent skin contact. Examples:- T-shirts
- underwear
- sportswear
- casual clothing
Product Class III – Limited Skin Contact
Garments with minimal direct skin exposure. Examples:- jackets
- coats
- outerwear
Product Class IV – Decorative Materials
Textiles primarily used for decorative purposes such as curtains or upholstery fabrics.Know the Restricted Substances Labs Screen For Commonly Found in Textiles
During professional fabric chemical testing, laboratories screen textile materials for a wide range of potentially harmful substances. Some of the most common chemicals tested include: Formaldehyde A chemical used in textile finishing processes that may cause skin irritation if present in high concentrations. Azo Dyes Certain azo dyes can break down into carcinogenic compounds and are restricted in many markets. Heavy Metals Metals such as lead, cadmium, and chromium may remain in dyed fabrics. Phthalates Plasticizers sometimes used in textile coatings and printed materials. Testing helps ensure that these substances remain within internationally accepted safety limits.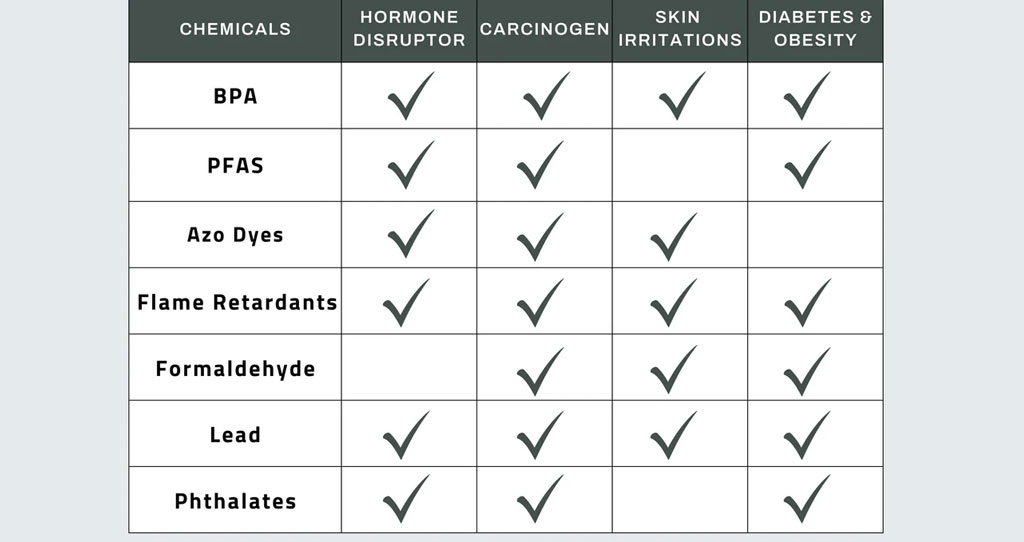
How to Run Safety Testing Before Bulk Production
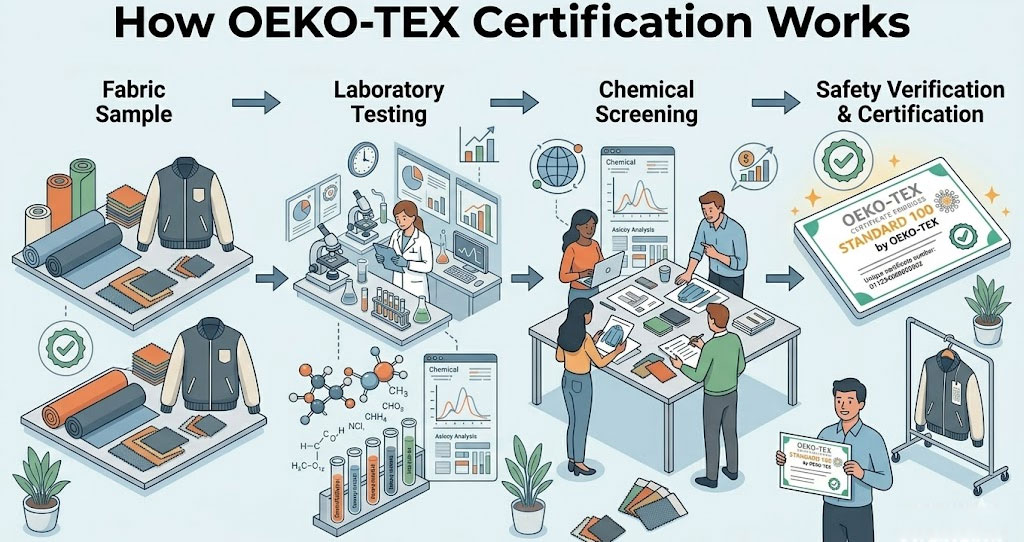
Fabric safety testing typically follows several standardized steps:- Fabric samples are submitted to professional laboratories
- Chemical screening identifies restricted substances
- Additional tests evaluate pH levels and colorfastness
- Results are reviewed against international safety standards
- Certified products receive official approval documentation
Global Textile Safety Regulations
In addition to voluntary certifications, apparel brands must comply with government regulations that restrict hazardous chemicals in consumer products. Important regulatory frameworks include:- REACH Regulation in the European Union
- Consumer Product Safety Improvement Act in the United States
OEKO-TEX vs Other Textile Certifications
While OEKO-TEX focuses primarily on chemical safety, several other certification systems address sustainability and responsible manufacturing practices.| Certification | Main Focus |
| OEKO-TEX | Chemical safety in textile products |
| Global Organic Textile Standard | Organic fibers and sustainable processing |
| bluesign | Responsible chemical management in production |
How Apparel Manufacturers Ensure Fabric Compliance
Professional clothing manufacturers usually implement strict quality control procedures to ensure textile safety and regulatory compliance. Typical compliance measures include:- Working with certified fabric suppliers
- Maintaining a Restricted Substance List (RSL)
- Conducting third-party laboratory testing
- Inspecting materials before production
- Performing quality checks before shipment
FAQ
1.What’s the difference between Standard 100 and STeP?
OEKO-TEX Standard 100 certifies that textile products are tested for harmful substances, while OEKO-TEX STeP evaluates the sustainability and environmental performance of manufacturing facilities.2.Do trims, prints, and labels need testing under Standard 100?
Yes. Under OEKO-TEX Standard 100, all components of a product—including trims, prints, labels, and sewing threads—should comply with the harmful substance limits.3.What documents should a supplier provide for retailer compliance?
Typical documents include the OEKO-TEX Standard 100 certificate, third-party test reports, material composition declaration, RSL compliance statement, and batch traceability records.4.How often should brands retest materials during bulk production?
Testing frequency usually depends on risk management: new materials or suppliers are tested more frequently, while stable materials may be retested periodically or through random inspections.5.Can recycled fabrics pass OEKO-TEX Standard 100?
Yes. Recycled fabrics can pass OEKO-TEX Standard 100 as long as they meet the same harmful substance limits as conventional textiles.Work With a Reliable Apparel Manufacturing Partner
For clothing brands, startups, and wholesale buyers, selecting the right manufacturing partner is essential for ensuring product safety and regulatory compliance. A professional apparel manufacturer should be able to provide:- Fabric certification documentation
- Third-party testing reports
- Transparent sourcing information
- Reliable quality control systems
Written by the Simmerui Textile Testing Team. We support B2B apparel brands with fabric safety screening, performance validation, and compliance documentation workflows. Our process typically includes RSL alignment, supplier certificate review, third-party lab coordination, and incoming material checks to help reduce chemical risk and ensure consistent bulk production quality for global retail requirements.